Safety · HSSE Watch
Aircraft Engine Sealant: Precision Maintenance Protects Integrity
Published
Occurrence: 31 July 2025 · TSB report released: 23 October 2026 · Worksite Safety Hub article published: 25 October 2026
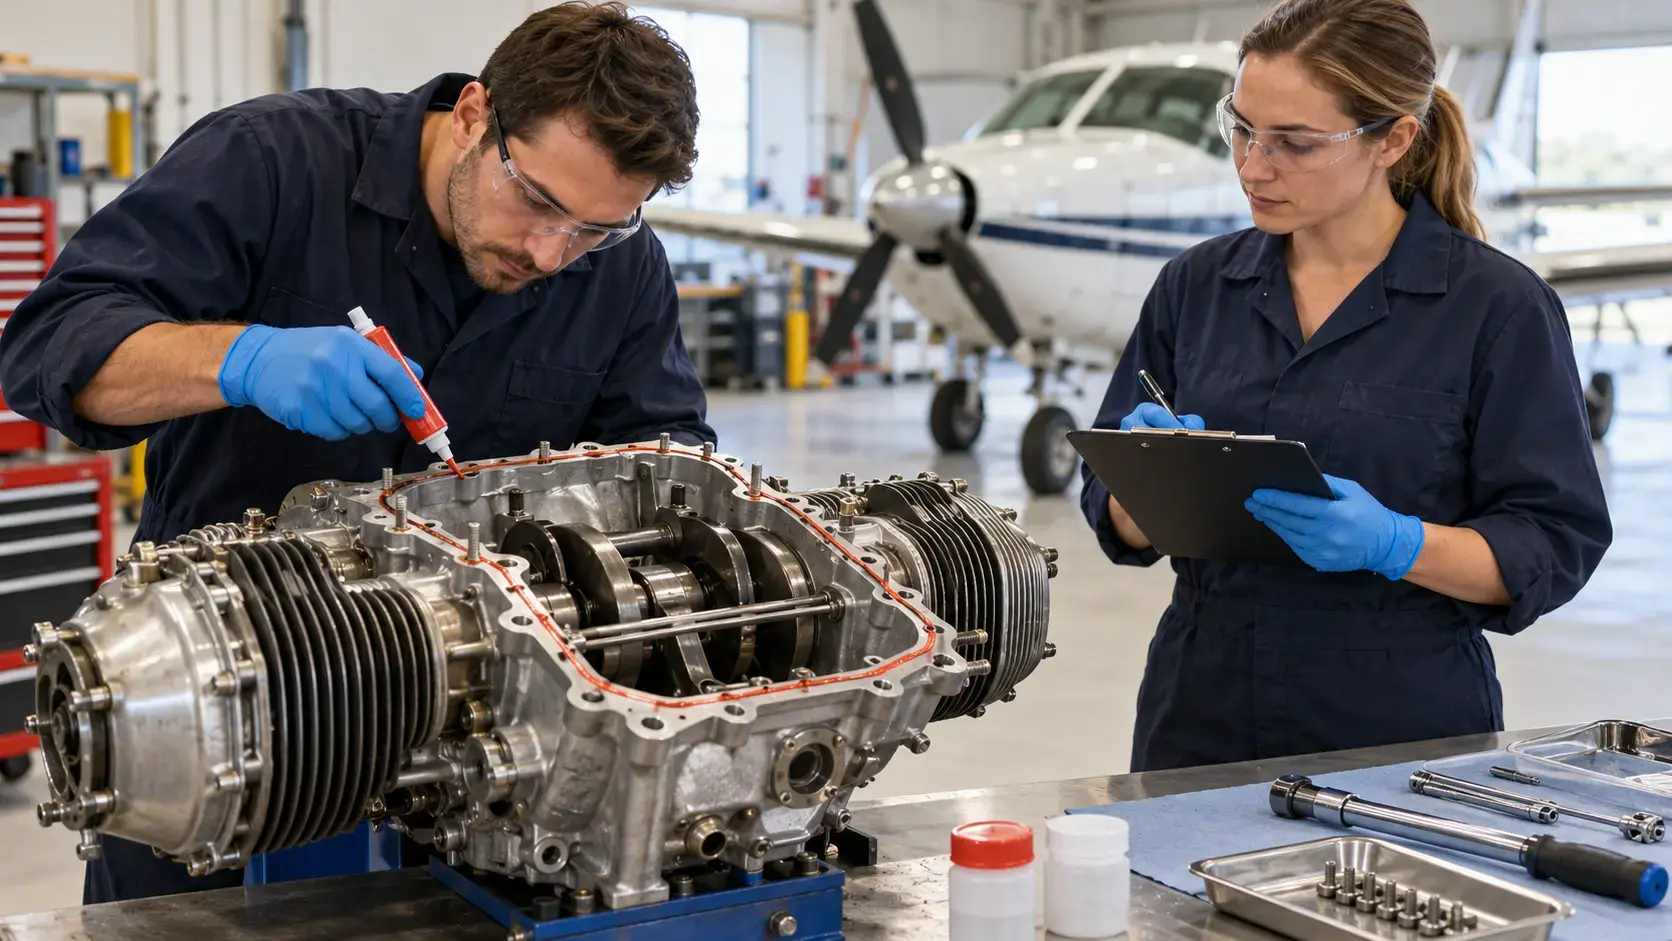
A sealant is not “just a consumable” when it can affect bearing seating, fastener friction, oil flow and structural clamping. A newly released Canadian investigation shows why precision assembly instructions, torque control, configuration verification and post-maintenance monitoring must work as one safety system.
What the investigation established
The Transportation Safety Board of Canada report A25O0114 ↗ was officially released on 23 October 2026. It covers the 31 July 2025 accident involving a privately registered Grumman AA-5A near Ottawa/Macdonald-Cartier International Airport.
During flight, the engine cowling opened, pieces detached and engine oil covered the windshield. The aircraft ultimately collided with trees short of the runway. The pilot was fatally injured and two passengers sustained minor injuries. TSB states that its role is to advance transportation safety, not assign civil or criminal liability.
The engine teardown found the No. 3 connecting rod failed, followed by fracture of the camshaft. TSB concluded that the engine failure was likely caused by misapplied LOCTITE-515 sealant. Sealant was found beyond the manufacturer-specified application area, including through-bolt surfaces and main-journal-bearing interfaces.
Why sealant location changed the risk
TSB explains that sealant on bearing interfaces could prevent correct seating and create material that might detach, migrate and interfere with engine operation. Sealant contacting through-bolt threads could produce an apparently normal torque reading while the actual clamping force remained too low.
In other words, the number on the torque tool was not enough. Friction conditions at the fastener had changed. TSB found that the reduced clamping force likely allowed unintended movement between the crankcase halves, abnormal operation of cylinder No. 3 and ultimately engine failure.
This mechanism has wider relevance wherever assembly compounds, lubricants, thread treatments or contamination can alter the relationship between applied torque and achieved bolt preload.
Transport Canada's safety alert
Transport Canada Civil Aviation Safety Alert 2026-07 ↗, effective 16 July 2026, was issued during the investigation. It warns owners, operators and maintainers of Lycoming opposed-cylinder engines about potential engine failure from improper crankcase sealant application.
The alert identifies potential outcomes including oil starvation, fastener torque loss, bearing distortion, internal damage, crankcase cracking, structural failure, persistent leaks and reduced reliability. It recommends reviewing the current Lycoming service instruction with the maintenance provider, addressing discrepancies before further operation and ensuring assembly personnel understand the permitted boundaries and restrictions.
The alert reflected the evidence available when issued and said the direct cause had not then been conclusively established. The later final TSB report records the investigation's conclusion that misapplied sealant likely caused the failure. Keeping those publication stages separate avoids treating an interim warning as a final finding.
1. Treat sealant application as a safety-critical step
Identify the approved product, revision of the manufacturer instruction, permitted surfaces, prohibited interfaces, film thickness or application method, cure conditions and cleanliness requirements. Make these controls visible at the point of work.
Do not replace an exact technical instruction with “apply sparingly” or informal local practice. When an instruction is unclear, stop and seek guidance from the manufacturer or other authorised technical source.
2. Protect fasteners, bearings and flow paths
Before application, positively identify bolt holes, threads, bearing supports, oil galleries and internal edges that must remain free of sealant. Use suitable masking, controlled dispensing, lighting and magnification where the approved procedure supports them.
After application, inspect for squeeze-out, transfer or contamination before the assembly becomes inaccessible. Excess material should be handled only by the authorised procedure; improvising removal can introduce debris or damage a sealing surface.
3. Control the conditions behind a torque value
Torque is an indirect way of achieving clamping force. Thread condition, lubrication, sealant, coatings, reused hardware and tool accuracy all influence the result. The work instruction must define the required condition, sequence, stages and any re-torque provisions.
If a prohibited material reaches a load-carrying thread or seating surface, do not simply wipe what is visible and continue. Record the discrepancy, assess the affected components under approved data and repeat the necessary preparation and verification.
4. Use an independent close-up inspection
Place a hold point before crankcase closure or any equivalent irreversible assembly step. A competent second person should verify product identity, application boundary, clean prohibited areas, bearing seating, fastener preparation and completion of the torque sequence.
Evidence can include controlled work cards, signed hold points and photographs where permitted. The objective is not paperwork volume; it is proof that the critical physical condition existed before it was hidden.
5. Verify the whole modification, not only the repaired component
The TSB report also identified modification discrepancies involving the supplementary engine identification plate, tachometer red-line marking and a fuel placard that no longer matched the approved engine configuration.
After a modification, reconcile the physical equipment, technical records, operating limitations, placards and identification. A signed modification form does not by itself prove that every required configuration detail is present and correct.
6. Strengthen post-maintenance surveillance
Define enhanced checks after intrusive maintenance: oil pressure and temperature trends, leakage, abnormal noise or vibration, filter and screen findings, fastener security and any manufacturer-specified inspection interval. Establish stop criteria and an escalation path before returning the equipment to normal service.
TSB found metallic debris in the oil filter as well as other engine discrepancies. Organisations should ensure abnormal findings are assessed collectively rather than closed as isolated defects without considering a common assembly or integrity problem.
7. Keep emergency response aligned with approved procedures
The report also reinforces the importance of recognising a complete power loss, establishing the approved glide condition and considering a reachable forced-landing area. Operators should use the applicable aircraft flight manual or pilot operating handbook, training and emergency procedures; this article is not flight instruction.
Maintenance prevention and operational readiness are complementary barriers. Neither can compensate for the absence of the other.
Leadership and toolbox questions
- Which assembly compounds can alter fastener friction, bearing seating or flow paths?
- Are current manufacturer instructions available at the exact point of work?
- Which surfaces must remain completely free of sealant, lubricant or debris?
- What independent hold point occurs before the assembly is closed?
- Can our records prove both the torque sequence and the required thread condition?
- After a modification, who reconciles records, placards, limits and physical configuration?
- Which post-maintenance finding would stop operation and trigger a broader integrity review?
Video availability
No directly relevant authoritative video explaining TSB report A25O0114 or Transport Canada CASA 2026-07 was verified at publication. No unrelated accident footage has been embedded. Use the official written report, current manufacturer instructions and applicable regulatory requirements.
Sources and dates
- Transportation Safety Board of Canada — Investigation Report A25O0114 ↗Official final report released 23 October 2026. Primary source for the occurrence, engine examination, maintenance history, analysis, safety action and safety message.
- Transportation Safety Board of Canada — Investigation page A25O0114 ↗Official occurrence summary and report access for the 31 July 2025 accident near Ottawa/Macdonald-Cartier International Airport.
- Transport Canada — CASA 2026-07, crankcase parting-surface sealants ↗Effective 16 July 2026. Official alert for owners, operators and maintainers of Lycoming opposed-cylinder engines, with recommended review and reporting actions.
Sources checked 25 October 2026. Source statements and original practical applications are distinguished above. Always consult current official advice and applicable local requirements.
Share the lesson
Open the separate 9:16 Pinterest poster
Illustrative visual, not an actual incident or a technical procedure. HSSE TIPS branding appears only in the designed poster footer.
Your experience matters
Share your thoughts on this page
Have a question, a useful experience or a suggestion? Add your input below.
Comments are public. Keep them respectful and relevant. Do not share contact details, confidential information or emergency reports.
Comments on this page
Loading comments…