Process Safety · Lesson 28 · 7 min read
A Valve Position Signal Does Not Prove the Flow Path
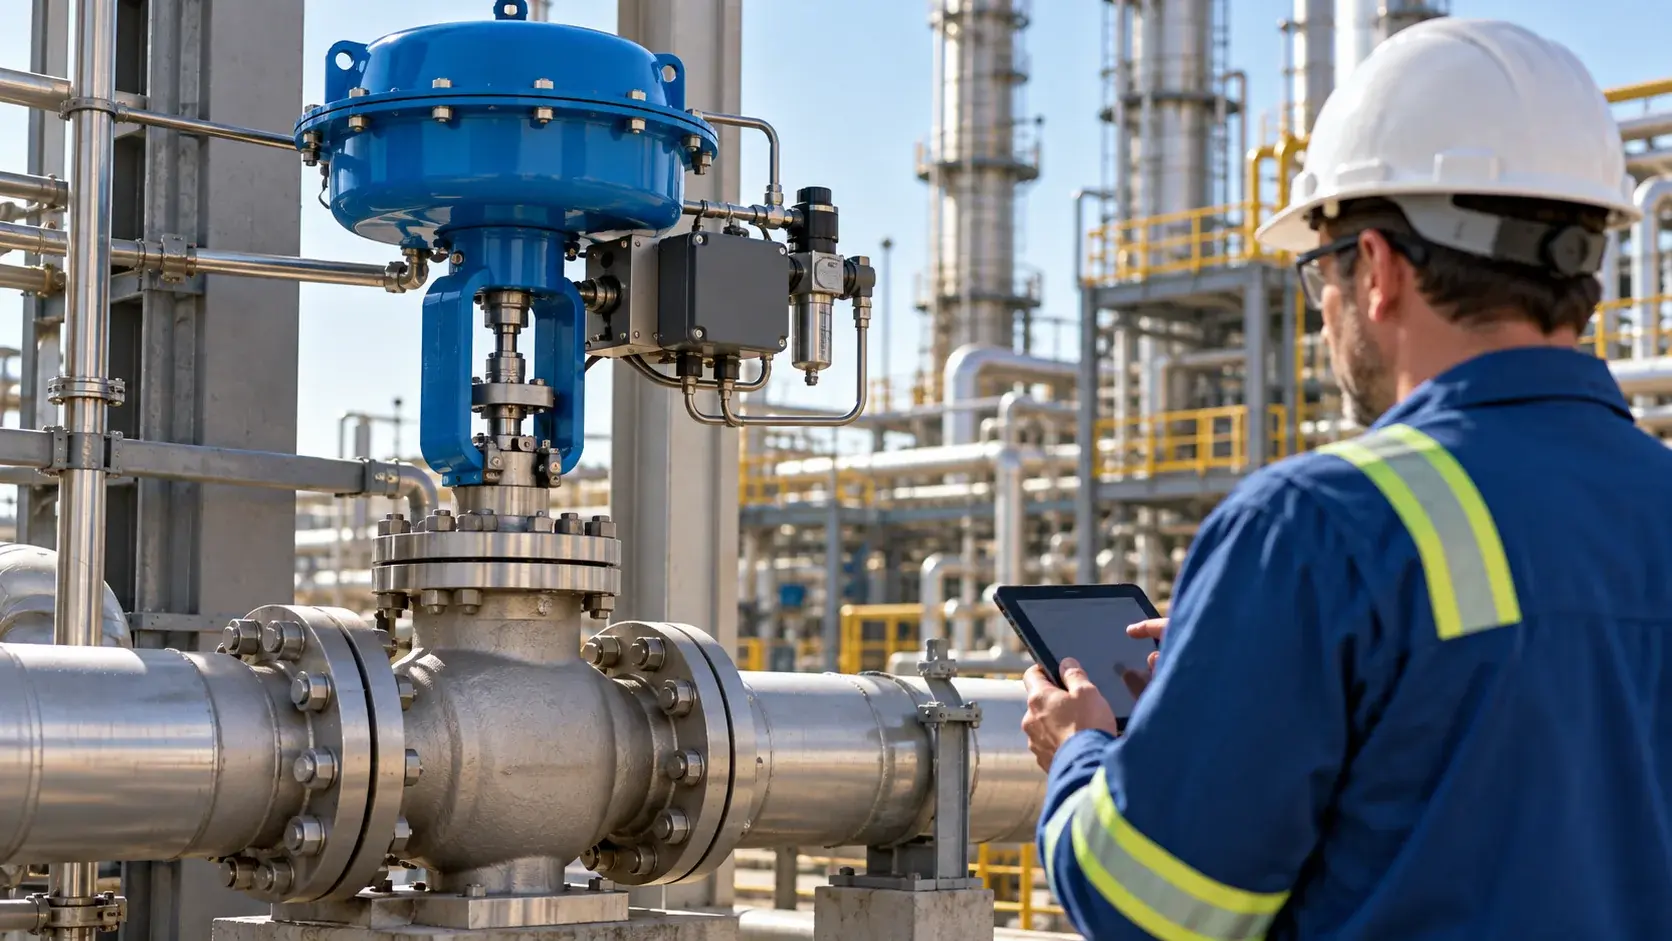
A green “closed” indication can describe the position of a switch, actuator or stem while the required process function remains unproven. The valve may be passing, mechanically disconnected, obstructed, installed with an unsuitable trim or exposed to a differential pressure greater than the actuator can overcome.
Why the hazard can remain hidden
Safety depends on the complete isolation function: detection of the demand, logic action, power or stored energy, actuator movement, mechanical connection, valve internals, seat performance and the process arrangement around the valve. Feedback from only one point in that chain can create false confidence.
The distinction matters most where rapid isolation limits the quantity of hazardous material released. Closing time, fail position, leakage performance and the ability to operate under realistic process differential pressure may all be performance requirements. A workshop stroke test or a limit-switch check may not demonstrate them.
A practical operating scenario
Hypothetical example: A remote shutdown valve receives a close command during testing and the control-room symbol changes state. Field verification finds that the actuator moved but the coupling has excessive play and downstream pressure decays much more slowly than expected. The indication was correct about the switch; it was incomplete evidence of the isolation function.
Critical controls
Understand the dependency. Define the required performance. State what the valve must isolate, its demanded position, maximum closure time, acceptable leakage, motive-energy requirements and the process conditions under which it must work.
Verify the barrier. Test the full function at a justified interval. Include command path, actuator, mechanical travel, feedback, closure time and appropriate evidence of isolation performance. Manage any limitations of testing under live conditions through a competent engineering basis.
Control the operation. Respond to discrepancy. Unexpected pressure equalisation, slow decay, unusual actuator behaviour or conflict between indications should be treated as a potential barrier impairment. Apply operating restrictions and escalation until the actual condition is understood.
What strong leadership looks like
Remote isolation valves are installed because people may not be able to approach safely after a release. Their reliability deserves visible ownership, clear performance standards and corrective action when proof tests reveal degradation.
Supervisors should make the current barrier status visible at handover, connect related defects and deviations, and ensure that temporary operating arrangements have clear limits and escalation triggers. Where required evidence is missing, the conservative response is to stabilise the process and seek competent support rather than allow schedule pressure to decide.
Actions for today
- Choose one relevant safety-critical function and trace it from process hazard to final protective action.
- Check the latest inspection, test or operating evidence—not only the design intention or status label.
- Resolve any discrepancy through the approved defect, risk-assessment and escalation process.
Learn from every test
Proof-test results should be trended rather than filed as isolated pass-or-fail records. Slower travel, increasing seat leakage, repeated adjustment or dependence on manual assistance can show deterioration before the function is lost. Confirm that test conditions represent the real demand as closely as practicable, including differential pressure and motive-energy availability. Where a full online test is not possible, document the limitation, use justified supplementary evidence and ensure the residual uncertainty is understood by the person accepting continued operation.
Team discussion question
For our highest-consequence remote isolation valve, what does the control-room indication truly confirm—and what separate evidence proves that flow will be isolated on demand?
Your experience matters
Share your thoughts on this page
Have a question, a useful experience or a suggestion? Add your input below.
Comments are public. Keep them respectful and relevant. Do not share contact details, confidential information or emergency reports.
Comments on this page
Loading comments…